
Process Technology · Scrubber Automation
Custom PLC Engineering and Remote Support for Wet Gas Scrubbers
How a purpose-built control system and secure remote access keep a scrubber performing, from commissioning through continuous operation.
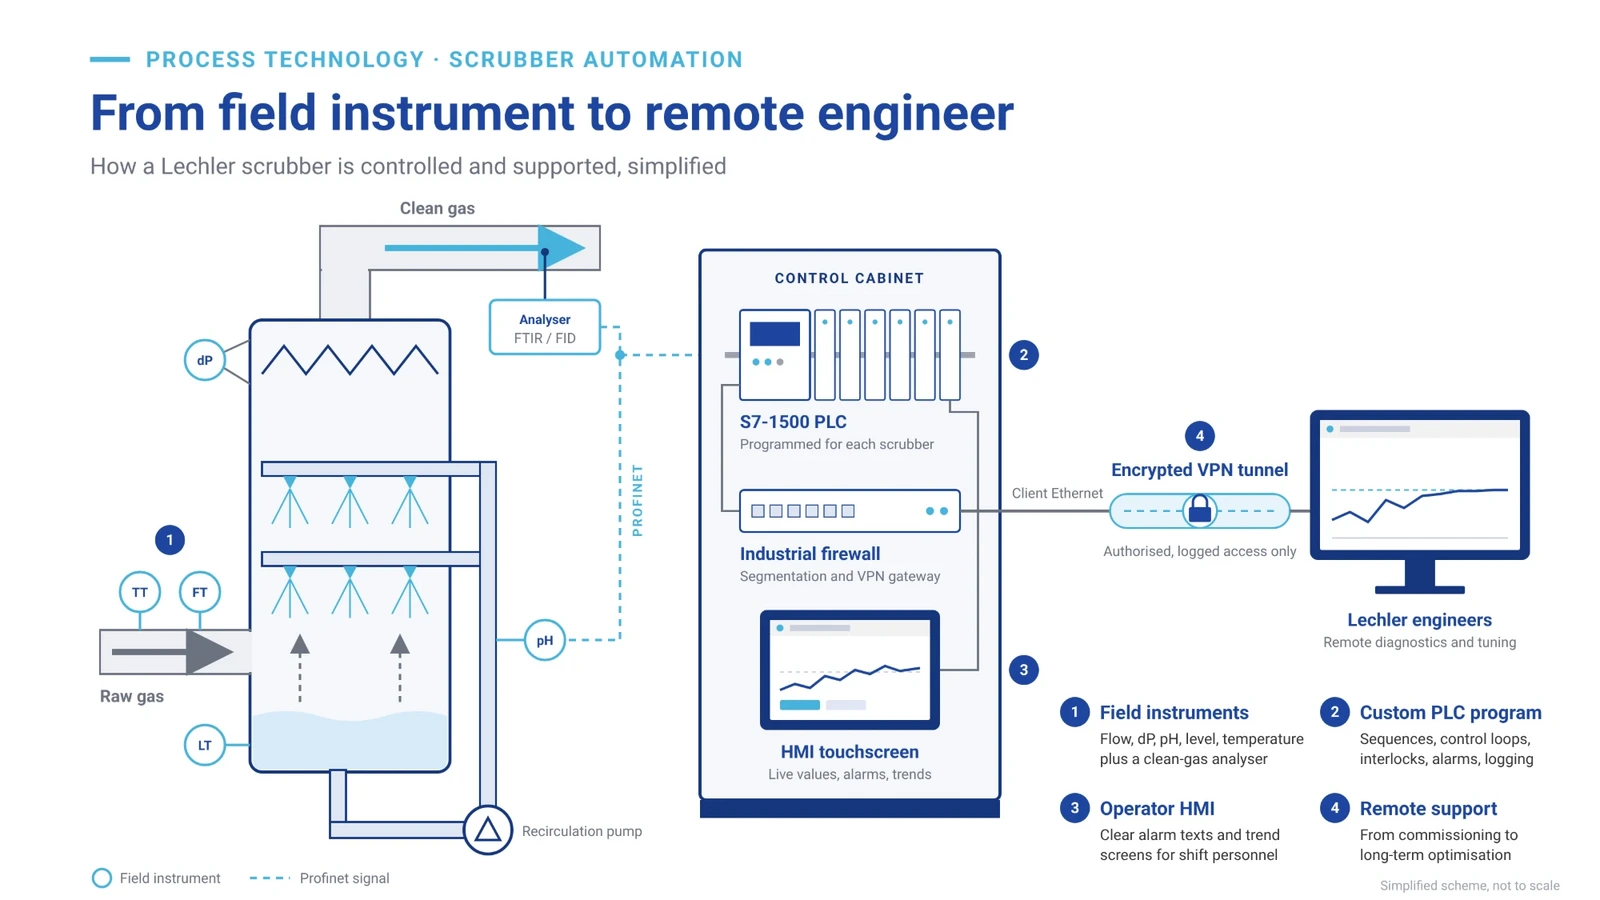
A wet gas scrubber is more than a vessel with spray nozzles. The automation layer, meaning the PLC, the operator interface, the field instruments and the engineers who keep it tuned, decides whether a scrubber is a reliable emission control asset or an unpredictable one. Every Lechler scrubber is therefore delivered with a control system engineered for that specific installation, and with secure remote support built in from day one.
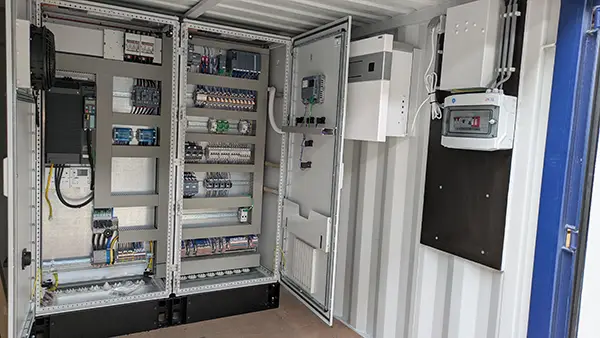
Lechler programs each control system for the scrubber it governs, on a Siemens S7 platform in a dedicated Rittal cabinet with Profinet field communication. A touchscreen HMI gives operators clear alarms and trends. A rugged Fortinet industrial firewall in the cabinet protects the control system and provides the encrypted VPN tunnel through which Lechler engineers support the installation remotely: during commissioning, when the impact is greatest, and throughout its operating life.
01 Purpose-built PLC engineering
No two industrial processes are identical, so no two Lechler control programs are either. Each one is written for the scrubber it governs, including multi-column and multi-stage systems, and also manages the auxiliary equipment around it: pumps, fans, dosing systems, valves and safety devices.
Siemens S7-1500, or S7-1200 for smaller scopes, programmed in TIA Portal
Dedicated Rittal control cabinet
Profinet, for deterministic, high-speed control of all instruments and actuators
Connection to a higher-level control system or DCS through standard industrial protocols
What a custom PLC program delivers
Automated start and stop
Smooth, repeatable ramp-up and shutdown sequences without operator intervention.
Closed-loop process control
Continuous adjustment of liquid flow, pH dosing and temperature to keep scrubbing conditions within specification.
Interlock logic
Automatic protective trips on abnormal pressure, loss of flow or chemical deviation.
Alarm management
Tiered alerts for early warning, operational deviation and safety shutdown.
Data logging
Time-stamped process values stored locally for trending, auditing and proof of performance.
Depending on the process, the PLC monitors and controls:
02 Hazardous gases and analyser integration
Where hazardous substances such as hydrogen cyanide (HCN) or flammable solvents are involved, the PLC and cabinet can be specified to ATEX zone requirements, with Ex p (pressurised) enclosures and intrinsically safe field loops.
Inline FTIR or FID analysers can be integrated into the control system. They close the loop between the measured outlet concentration and the control response, and they document emission performance continuously. Read more about emission control with analysers.
With an analyser in the loop, the scrubber is controlled on what actually leaves the stack, not only on indirect values such as pH and conductivity.
03 The operator interface
The HMI is the window into the scrubber's live process state. Lechler installs touchscreen HMIs that show all critical parameters at a glance: gas flow, liquid circulation, differential pressure over the droplet separator, sump level, pH and temperature.
Alarms appear as clear, actionable text rather than fault codes, so shift personnel can respond decisively without consulting a manual. Trend screens show the last hours or days of operation, which helps operators spot process drift before it becomes a problem, for example during seasonal changes in inlet gas composition or production throughput.
04 Secure remote support and monitoring
Every Lechler scrubber control cabinet is equipped with a rugged Fortinet industrial firewall as standard. It has two roles at once: it protects the control system, and it establishes the encrypted channel through which Lechler engineers support the installation remotely.
Cybersecurity
The firewall enforces network segmentation and access control according to security policies agreed with the client. Only authorised Lechler engineer credentials can open a session, and every access is logged.
VPN connectivity
A secure VPN tunnel connects the site to the Lechler engineering team for PLC diagnostics, parameter adjustment and software updates, without travel to site.
Continuous optimisation
After commissioning, engineers follow process trends and fine-tune control loops, setpoints and interlock thresholds to improve separation efficiency and availability.
Fast troubleshooting
Many faults can be diagnosed, and often resolved, without a site visit. That shortens downtime, especially in the first weeks of operation.
05 Making the connection
Because PLC software changes during commissioning are made remotely, connectivity and cybersecurity need to be settled before the scrubber is delivered.
Engineering phase
Connectivity and security policies are agreed with the client's IT or OT department.
Before delivery
The client provides a wired Ethernet connection to the firewall in the control cabinet and arranges the network access authorisations. Industrial Wi-Fi can be used with prior approval; other options can be discussed during engineering.
Commissioning
Remote access is active from the first day of start-up, so Lechler engineers can follow live data from the very beginning.
06 Commissioning: where remote support counts most
The start-up of a new scrubber is the period of greatest risk and greatest opportunity. In the first weeks, process conditions often differ from the design assumptions: actual gas compositions vary, the liquid chemistry needs tuning, and control loops have to be tightened against the real process rather than a simulation.
With remote access active from day one, Lechler engineers can follow live data continuously, intervene as soon as deviations appear and adjust the control system in real time.
The result is a faster route to stable, compliant operation, and a scrubber tuned to its real process rather than to its design sheet.
07 Long-term operational support
Remote monitoring does not end at commissioning. Under an ongoing support arrangement, Lechler continues to watch the installation for performance drift, early signs of equipment wear and changing process conditions. As part of a structured service programme, the following can be delivered remotely:
- PLC software updates as the process or the requirements change
- Interlock revisions when operating limits are adjusted
- Control loop retuning to restore or improve separation efficiency
This reflects how Lechler works: not simply as an equipment supplier, but as an emission control partner with a stake in the continued performance of every system it delivers.
08 Applications
Custom PLC engineering and remote support are standard across the full Lechler scrubber range, including systems for:
- Acid gas removal (SO₂, HCl, HF), see sulphur dioxide
- Hydrogen cyanide (HCN) abatement in chemical and petrochemical processes, see cyanides
- Odour reduction (VOCs, ammonia, butyric acid), see odour nuisance
- Pyrolysis and waste-to-energy gas cleaning, see pyrolysis
- Flue gas desulphurisation
- Foam manufacturing emission control
- Methanol and solvent vapour abatement
Frequently asked questions
Does remote access expose our plant network?
No. The firewall in the control cabinet segments the scrubber's control network from the plant network, according to security policies agreed with your IT or OT department. Only authorised Lechler engineers can open a session, and every session is logged.
What if a wired connection is not available?
Industrial Wi-Fi can be used with prior approval, and other connectivity options can be discussed during the engineering phase. The connection has to be in place before commissioning.
Can the scrubber be connected to our DCS?
Yes. The scrubber runs as a stand-alone control system, and it can exchange status, alarms and process values with a higher-level control system through standard industrial protocols.
Can remote monitoring be added to an existing scrubber?
In many cases, yes. What is possible depends on the existing control system and cabinet. Lechler assesses this during an engineering review and proposes either an upgrade of the existing system or a new control cabinet.
Can the control system be used in ATEX zones?
Yes. For applications with flammable or toxic gases, the cabinet and field instrumentation can be specified to the required ATEX zone, with Ex p (pressurised) enclosures and intrinsically safe field loops.
Planning a new scrubber, or looking to add remote monitoring to an existing one? Our engineering team will help you define the control system and connectivity your process needs.