
Project Execution · EPC Turnkey
Complete project responsibility from start to finish. Lechler doesn't just deliver products; we deliver complete solutions, from the first process calculation to formal handover and beyond.
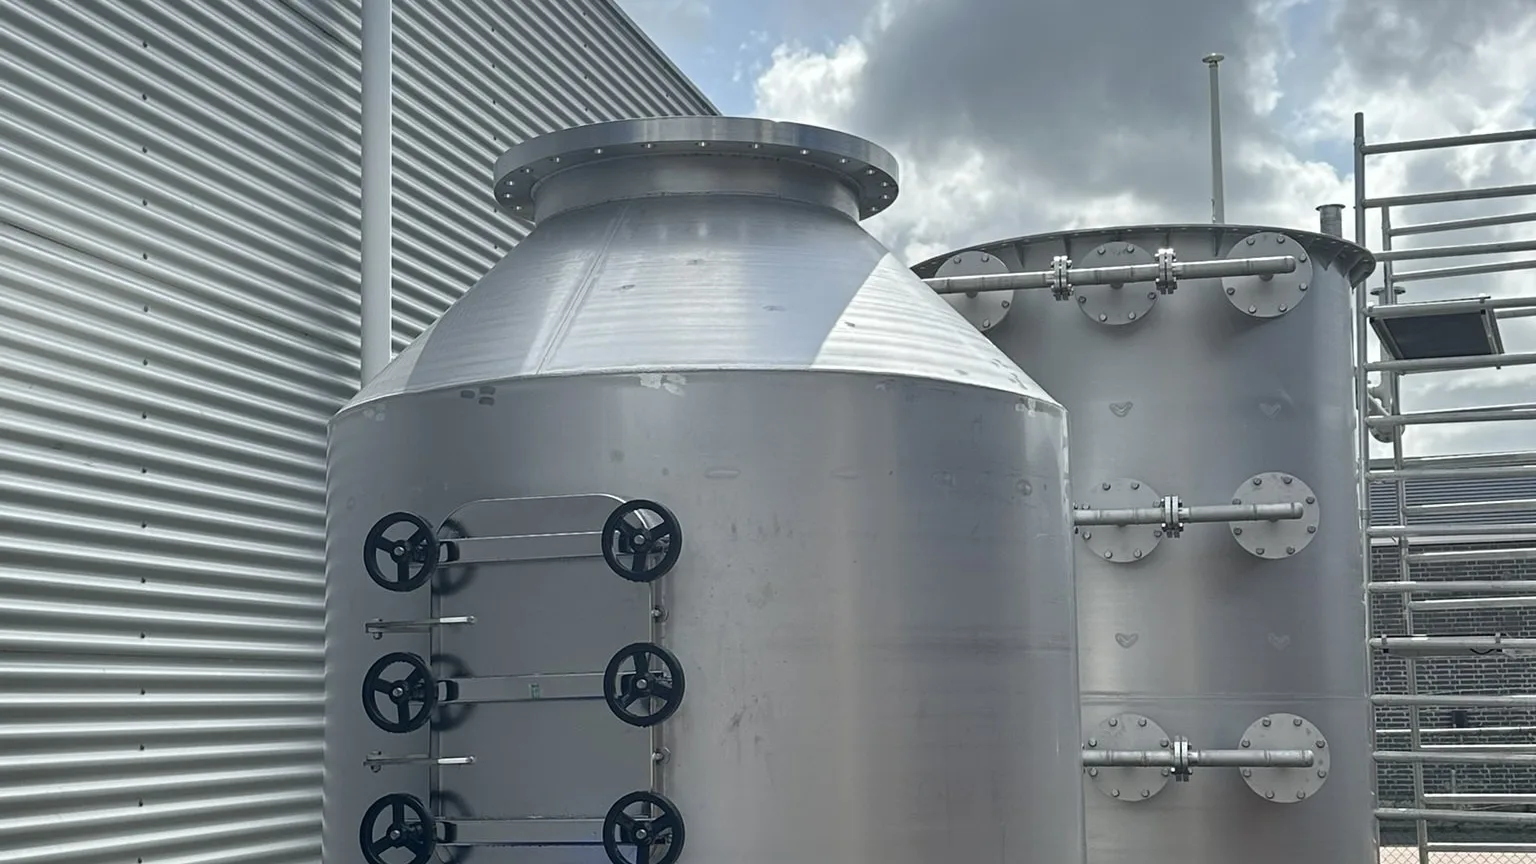
As an EPC turnkey contractor and Original Equipment Manufacturer in one, Lechler takes end-to-end responsibility for a gas scrubber project: process data, engineering, production, control systems, factory acceptance testing, installation, commissioning and service. This article walks through each phase, what the client receives at each step, and why one continuous line of responsibility reduces project risk.
01 One supplier, one responsibility
Industrial emission control demands precision, reliability and clear lines of accountability. In practice, projects involving several separate parties, each responsible for their own scope, frequently run into interface problems, delayed decisions and disputes over responsibility. The result is longer lead times, higher costs and uncertainty for the client.
Lechler addresses this by bringing the entire project under one roof. As an EPC turnkey contractor and Original Equipment Manufacturer in one, Lechler takes end-to-end responsibility: from the first process calculation through to formal handover. There is no gap between engineering and manufacturing, and no mismatch between design intent and commissioning.
0 Process data Inline measurement and evaluation at the client's site Where gas composition is unknown
- 1EngineeringProcess design, 3D design, calculation
- 2ProductionIn-house fabrication and welding
- 3ControlElectrical cabinets and PLC
- 4FATFactory acceptance test
- 5InstallationOn-site erection and integration
- 6CommissioningSAT, start-up, performance test
- 7ServiceMaintenance and remote support
One team · every skill · the total solution
02 From process data to engineering package
Analysing and evaluating process data
Where the gas composition entering the scrubber is unknown or insufficiently characterised, Lechler can carry out inline measurements with process analysers directly at the client's installation. These measurements give a real-world dataset of gas composition, pollutant concentrations and flow characteristics under actual operating conditions.
The data is then evaluated by our engineers and becomes the technical basis for absorber sizing, reagent selection and process design, so that the system is engineered to match reality, not assumptions. How such a measurement campaign works is described in Measuring an Unknown Emission.
Process engineering and engineering packages
All technical development is carried out in-house. Lechler performs mass transfer calculations, absorber sizing, liquid-to-gas ratio analysis, stress calculations and material selection based on corrosion resistance, operating temperature and chemical compatibility. Every engineering decision is made by the same team that will subsequently build and install the system.

Resource efficiency is part of the engineering from the outset. By optimising reagent consumption, liquid-to-gas ratio and energy input at the design stage, Lechler designs every system for the lowest resource consumption that still meets the required performance.
Minimising the use of water, absorption liquid, chemicals and energy is not an afterthought. It is a core engineering objective.
The engineering process produces a complete documentation package. All deliverables conform to the applicable international standards, including ASME, ASTM, API and ISO.
- P&IDs
- Functional descriptions
- Safety data sheets
- Motor and instrumentation lists
- 3D fabrication drawings
- Electrical drawings
- PLC programming
- ASME · ASTM · API · ISOApplicable standards
03 Procurement, fabrication and installation
Procurement and fabrication
Lechler manages the entire supply chain, from construction material to auxiliary equipment.
- Construction material
- Internal scrubber components
- Recirculation pumps
- Chemical dosing systems
- Heat exchangers
- Liquid filter systems
- Blowers
- Instrumentation
- Electrical and control systems
- Auxiliary equipment
Because core equipment and electrical cabinets are made in-house, Lechler keeps full quality control and traceability throughout fabrication. Welding procedures, non-destructive testing, surface treatment and factory acceptance testing (FAT) are all carried out within one quality management framework, without relying on third-party subcontractors for critical scope.
Site construction and installation
Lechler manages the complete site installation: mechanical erection, pipework, electrical and instrumentation works, and integration with upstream and downstream process units. Construction supervision, safety compliance and interface coordination are handled by the same team throughout this phase, which keeps the project aligned with the plant layout and the client's operational requirements.
04 Commissioning and performance testing
Project completion follows a structured commissioning programme. At each stage, the scrubber system is verified against its guaranteed parameters.
- 1Cold commissioningChecks and function tests without process gas
- 2Hot commissioningStart-up under real process conditions
- 3Site acceptance testSAT on site
- 4Performance testingVerification against guaranteed parameters
- ✓Formal handoverOnly when all criteria are demonstrably met
- Pollutant removal efficiency
- Outlet emission limits
- Pressure drop across the system
- Energy consumption
- Overall system availability
Process analysers for resource-efficient operation
A key element of modern scrubber commissioning is the integration of high-end process analysers. Lechler specifies and integrates analysers for continuous monitoring of gas composition, pollutant concentrations and absorption efficiency. They provide real-time data for precise, dynamic control of reagent dosing, liquid flow rates and other system parameters, which translates into savings in chemicals, water and energy during operation. See also Do You Really Know What Your Process Consumes?
Fixed set-points
- Conservative operating margins
- Risk of over-dosing reagents
- Unnecessary consumption of water, chemicals and energy
Analyser-based control
- Real-time data on gas composition and absorption efficiency
- Dynamic control of dosing, liquid flow and system parameters
- Continuous adaptation to actual process conditions
Formal handover only takes place once all performance criteria have been demonstrably met, so the client starts operation with a system that has proven its guaranteed values on site.
05 After handover: lifetime support
At handover, the client receives a complete documentation package. Long-term technical support remains available throughout the system's design life, for reliable and compliant operation of the scrubber well beyond commissioning. Our engineers can also support the installation remotely through the PLC; see PLC control and remote support.
- As-built drawingsThe system exactly as delivered
- Operation and maintenance manualsFor daily operation and servicing
- Operator training materialsFor the client's own personnel
06 Why integrated execution makes the difference
In traditional project structures, engineering, fabrication and installation are divided between separate parties. Each transition between disciplines is a risk: information is lost, assumptions diverge and the client is left to manage the interfaces.
Lechler removes these risk points. Because design, production and execution are in the hands of one organisation, technical decisions made during engineering carry straight through to fabrication and installation. There is no reinterpretation, no finger-pointing and no ambiguity over who is accountable when something needs to be resolved.
Traditional project structure
- Engineering firm, equipment supplier and site contractor each hold their own contract
- The client manages the interfaces between them
- Each hand-over between parties risks lost information, delay and disputes
Lechler integrated execution
- One contract and one team for engineering, fabrication, installation and commissioning
- Decisions made in engineering carry straight through to the site
- One point of accountability
Because every Lechler scrubber system is individually engineered and built to the requirements of each project, there are no constraints imposed by standardised, off-the-shelf configurations. Designing from first principles means Lechler can build current technology into every system, from process analysers and smart instrumentation to modern control architectures, regardless of scale or application. Clients get a solution tailored to their process rather than one limited by a fixed product range. Read more about our open spray scrubbers or, for an existing installation, Upgrade or Replace?
The result for the client:
- Reduced project risk
- Shorter lead times
- Measurable savings in resource consumption throughout the system's operational life
- A system that performs as specified from the moment it is handed over
Discuss your emission challenge with our engineers. Lechler Process Technology BV · 't Woud 59, 3232 LN Brielle, The Netherlands · +31 181 419 419